


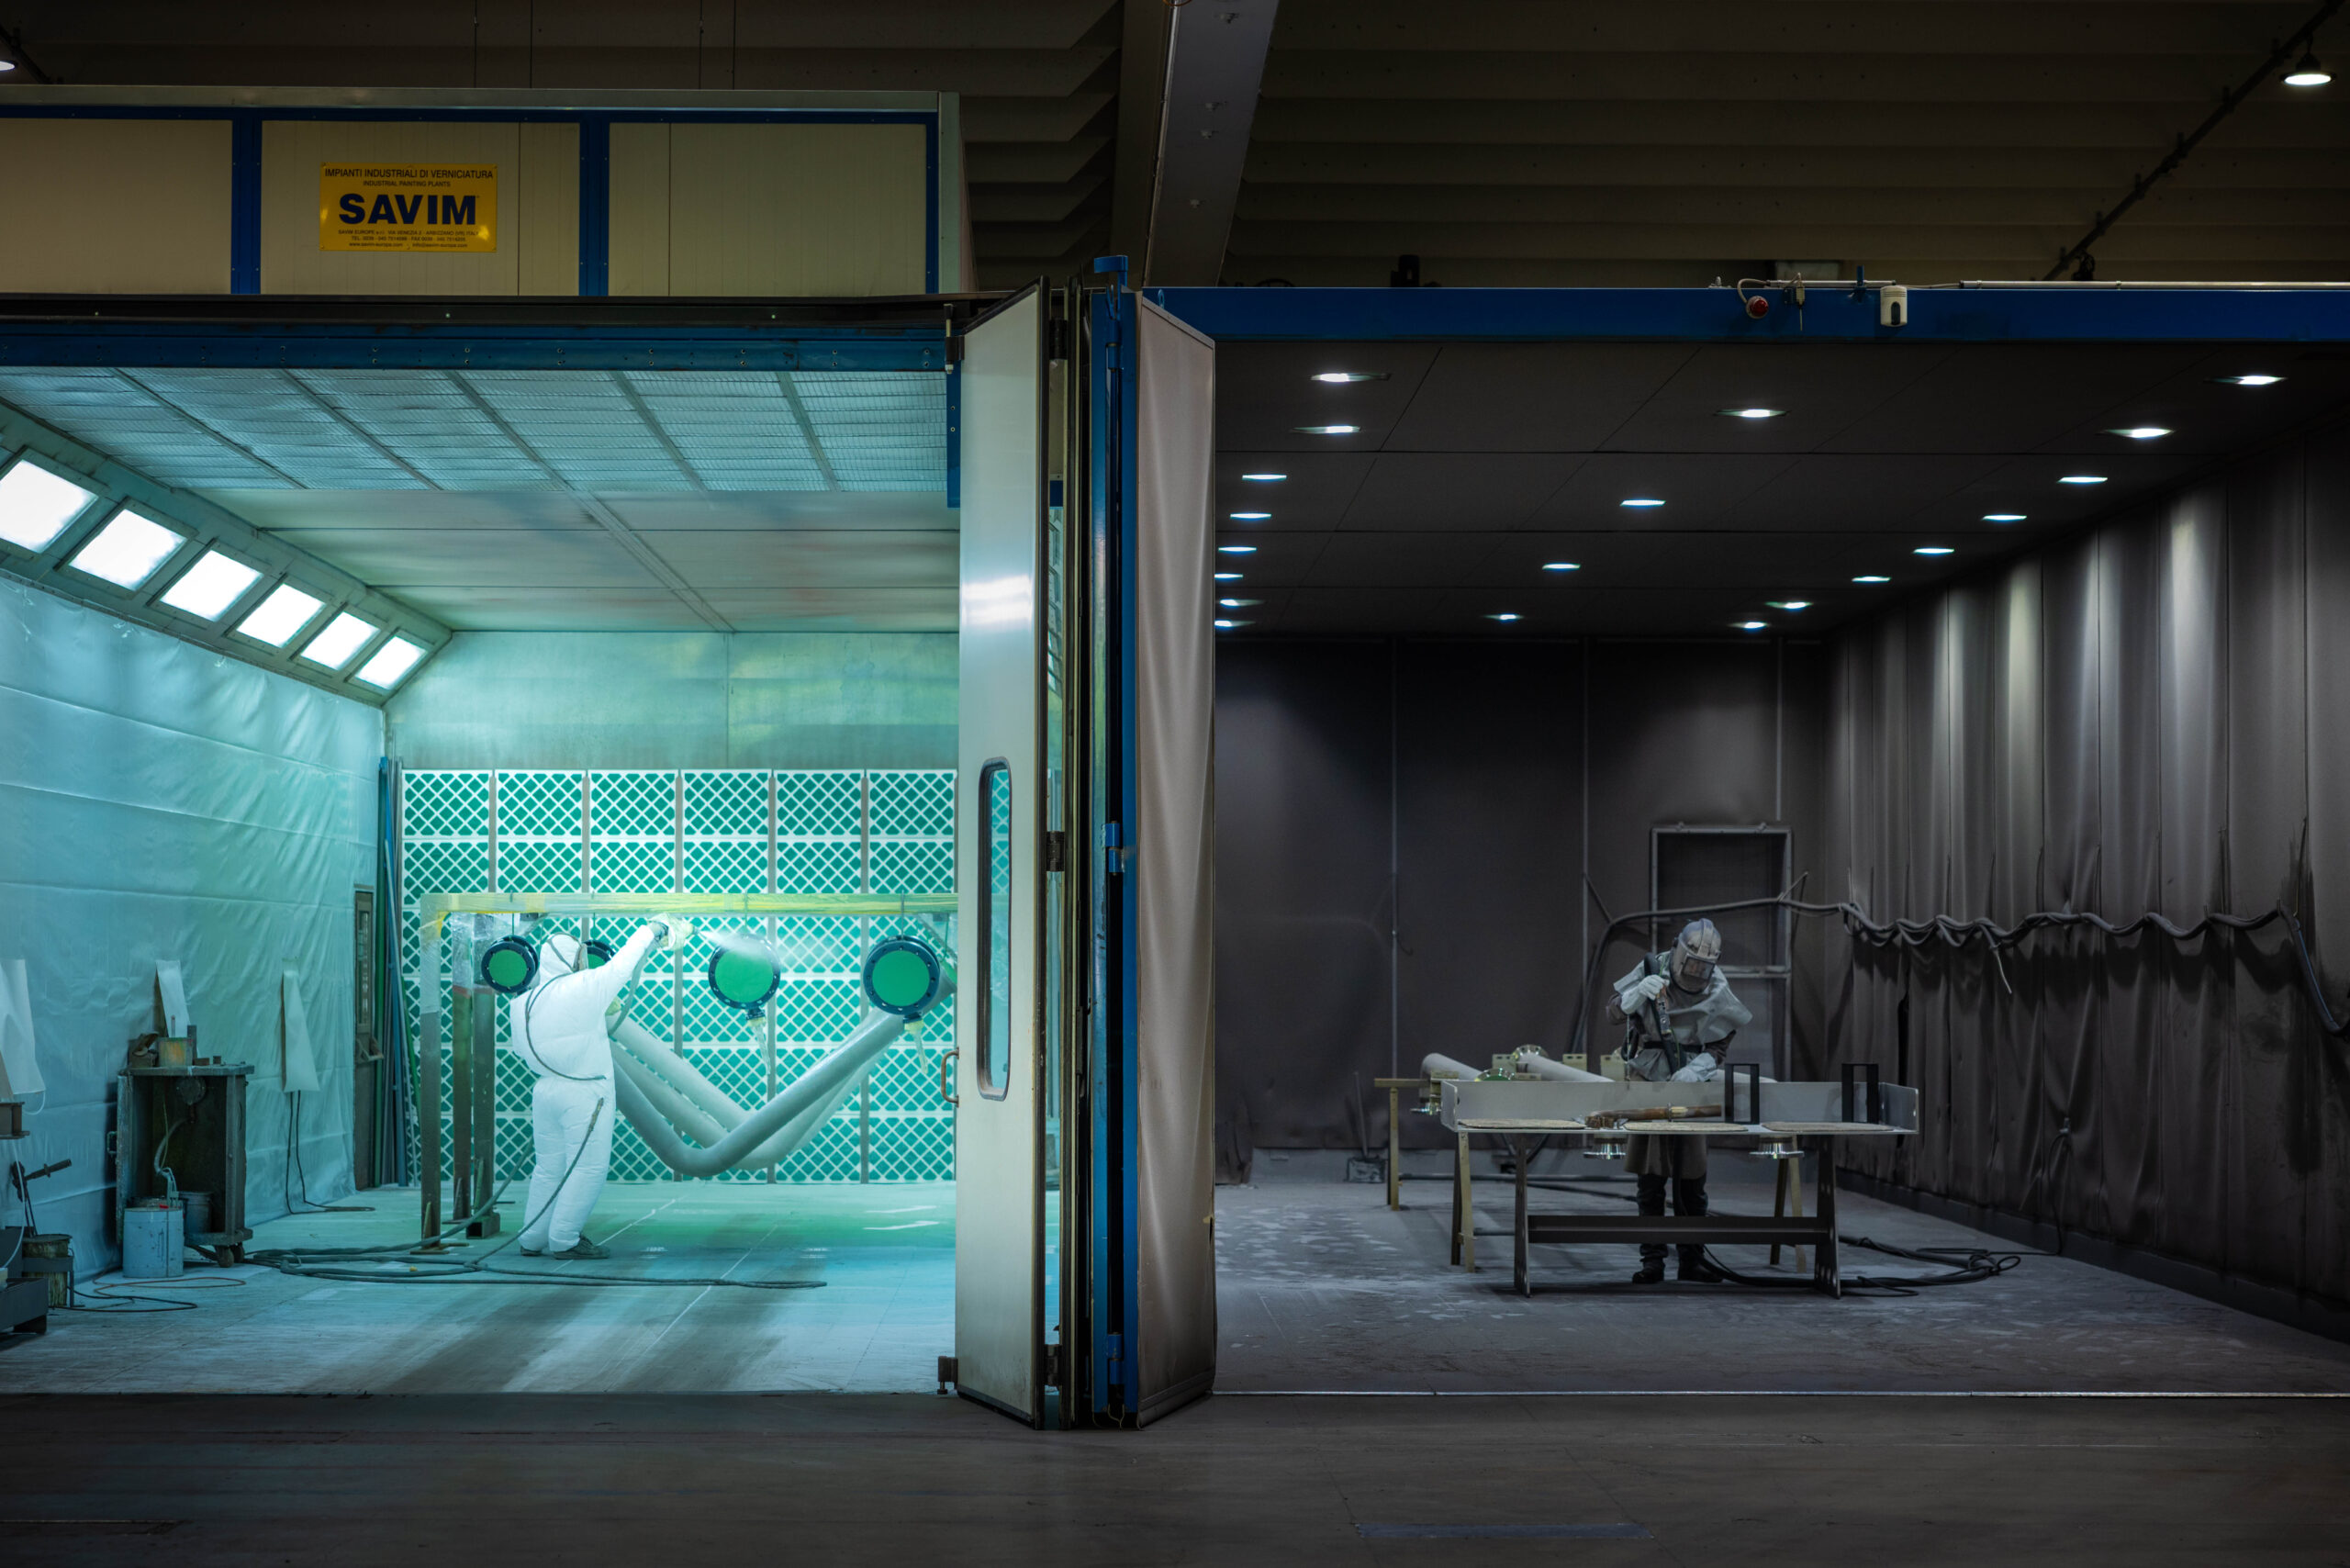
WE TAILOR OUR SYSTEMS TO YOUR NEEDS. BUT WHAT ARE THE KEY FACTORS THAT DRIVE CUSTOMIZATION?
THE CONTEXT
Instrument Air and Nitrogen Plants for the O&G industry mainly operate in harsh, corrosive environments, where surface preparation and protective coating systems are critical to long-term equipment integrity and durability.
Sinergia has developed the expertise and infrastructure to manage sandblasting and painting entirely in-house, achieving complete independence from external suppliers.
Controlling surface preparation, coating application, and complying with each project’s specifications, ensures reliable corrosion protection and consistent quality across all packages.
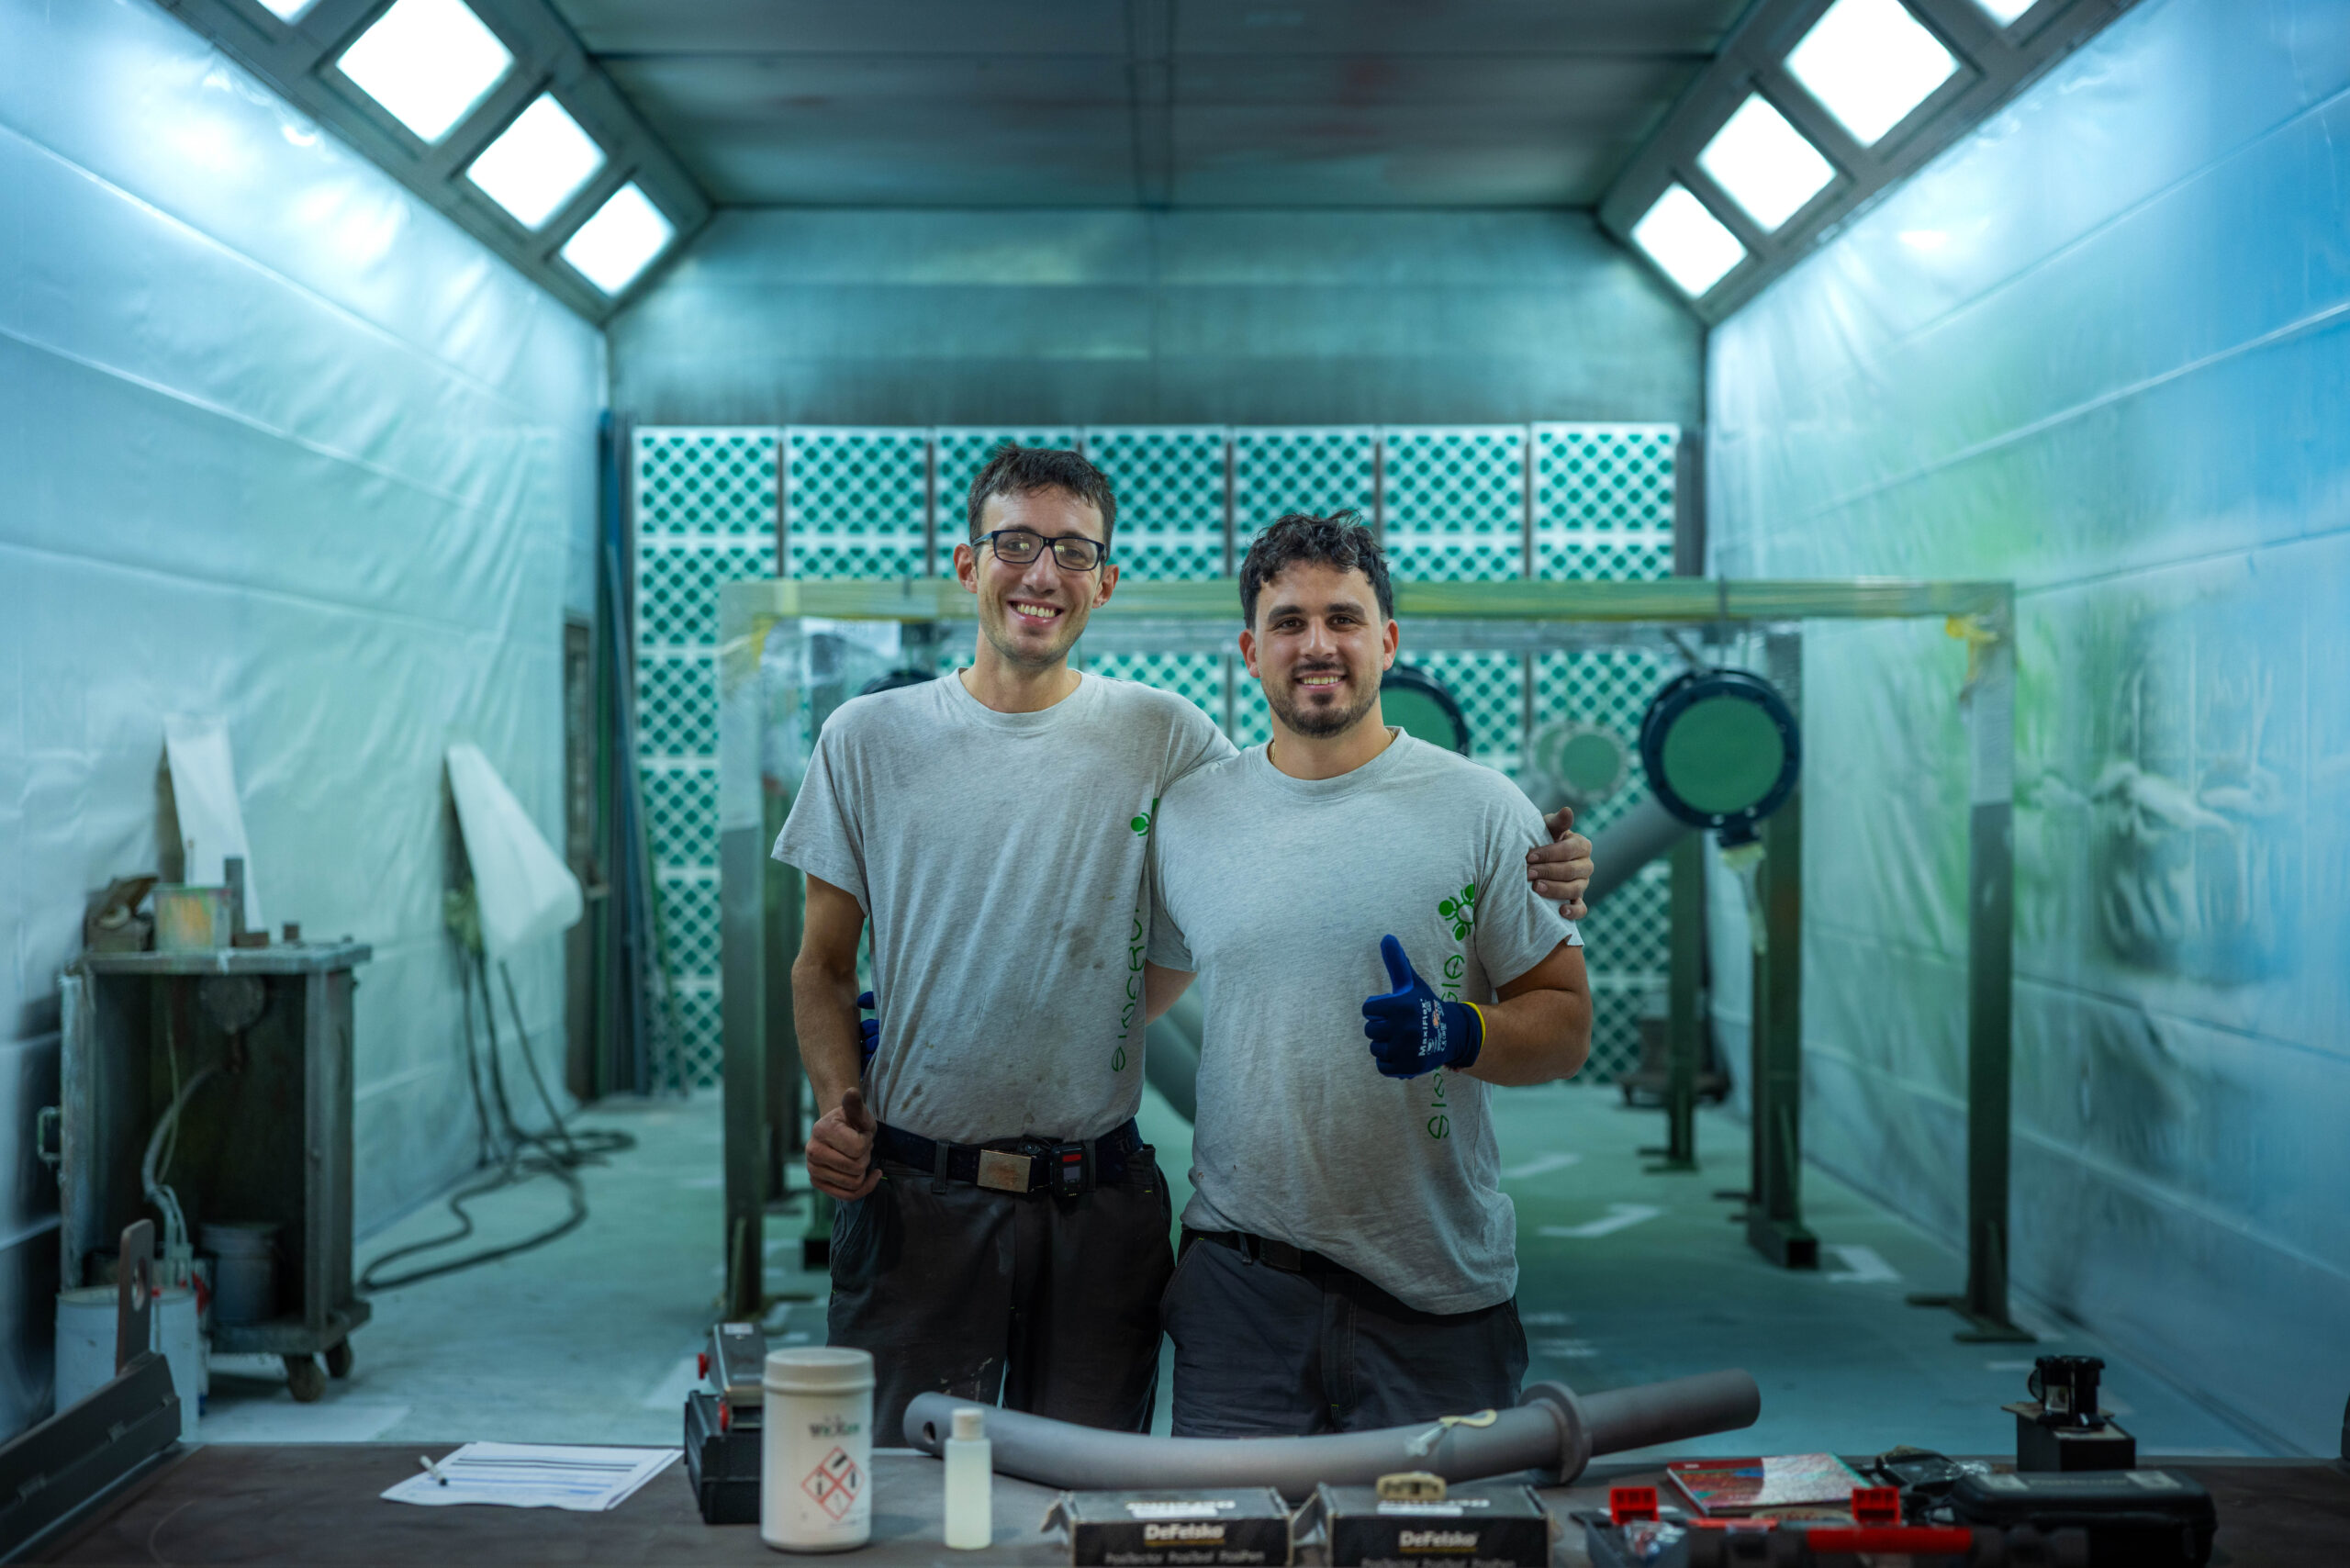
SANDBLASTING
The sandblasting process, which is managed by a dedicated team of four people, begins with an initial degreasing process using a solvent (often in accordance with specification NMS039) to remove any dirt and contaminants. Baseplates, structural frames, pressure vessels, pipes, canopy panels, together with minor elements undergo this phase.
The choice of technology and abrasive media for sandblasting depends on the material being treated. Metallic grit is typically used for carbon steel components, while corundum is preferred for stainless steel.
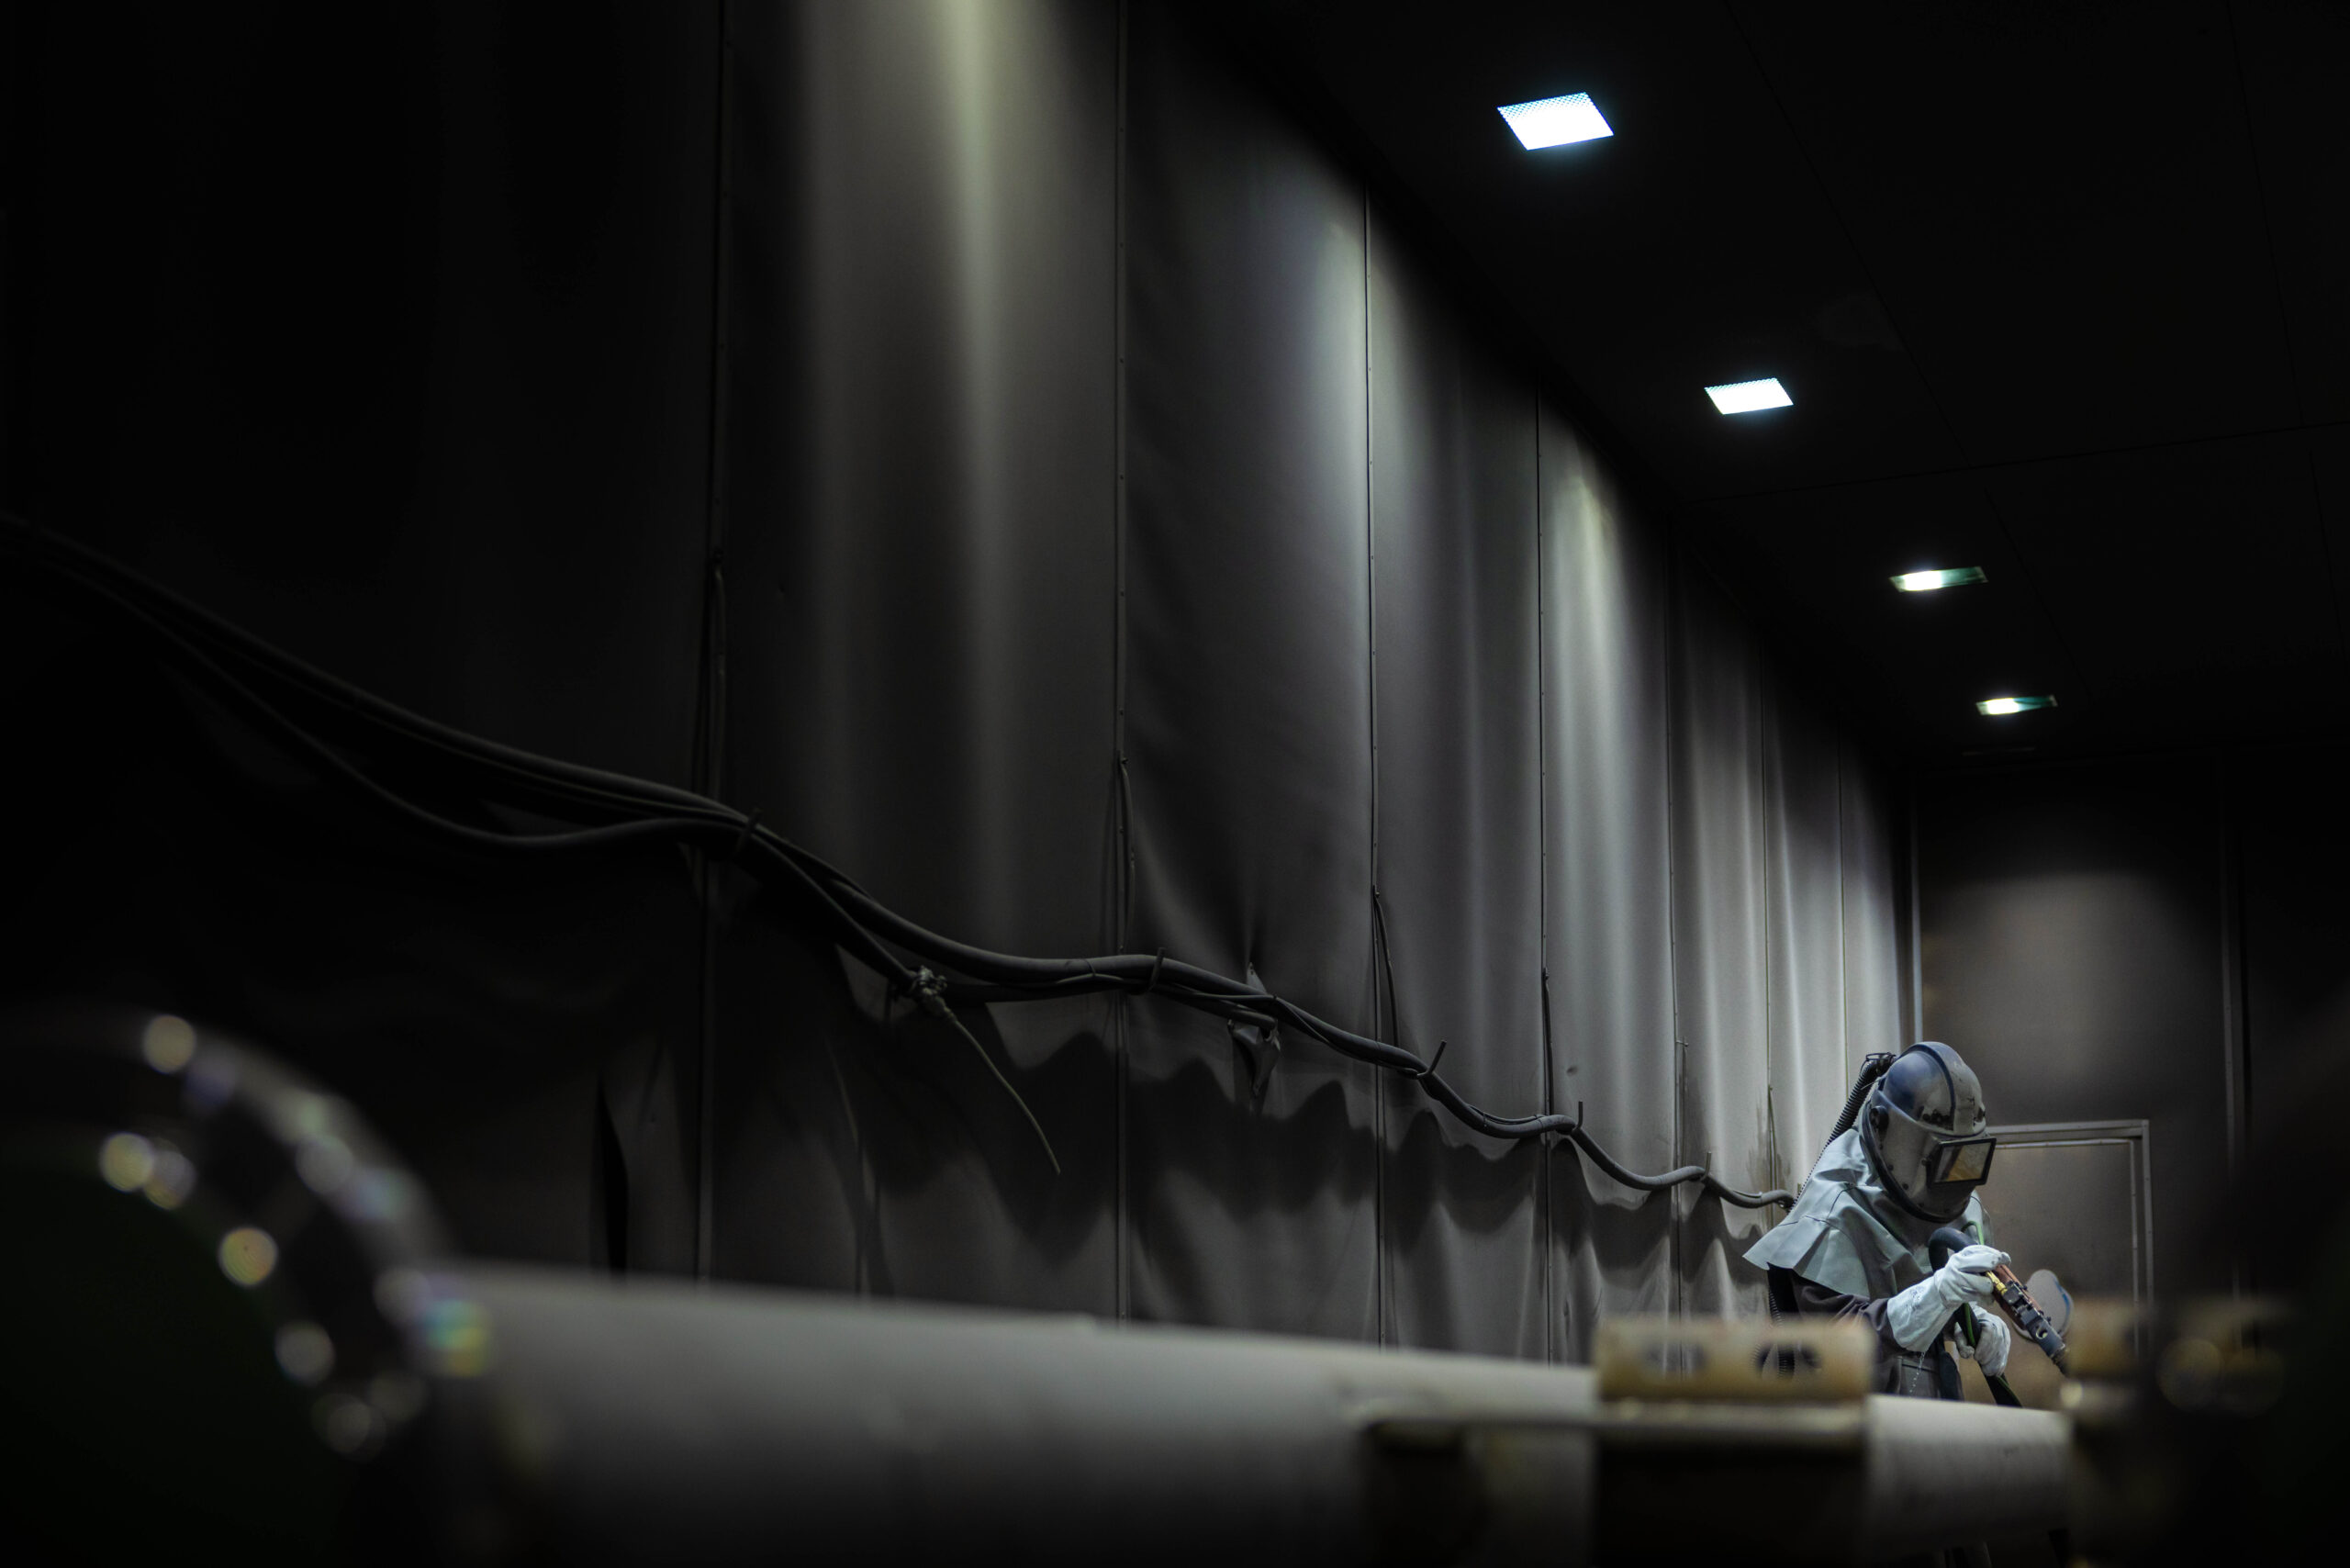
THE INITIAL TESTS
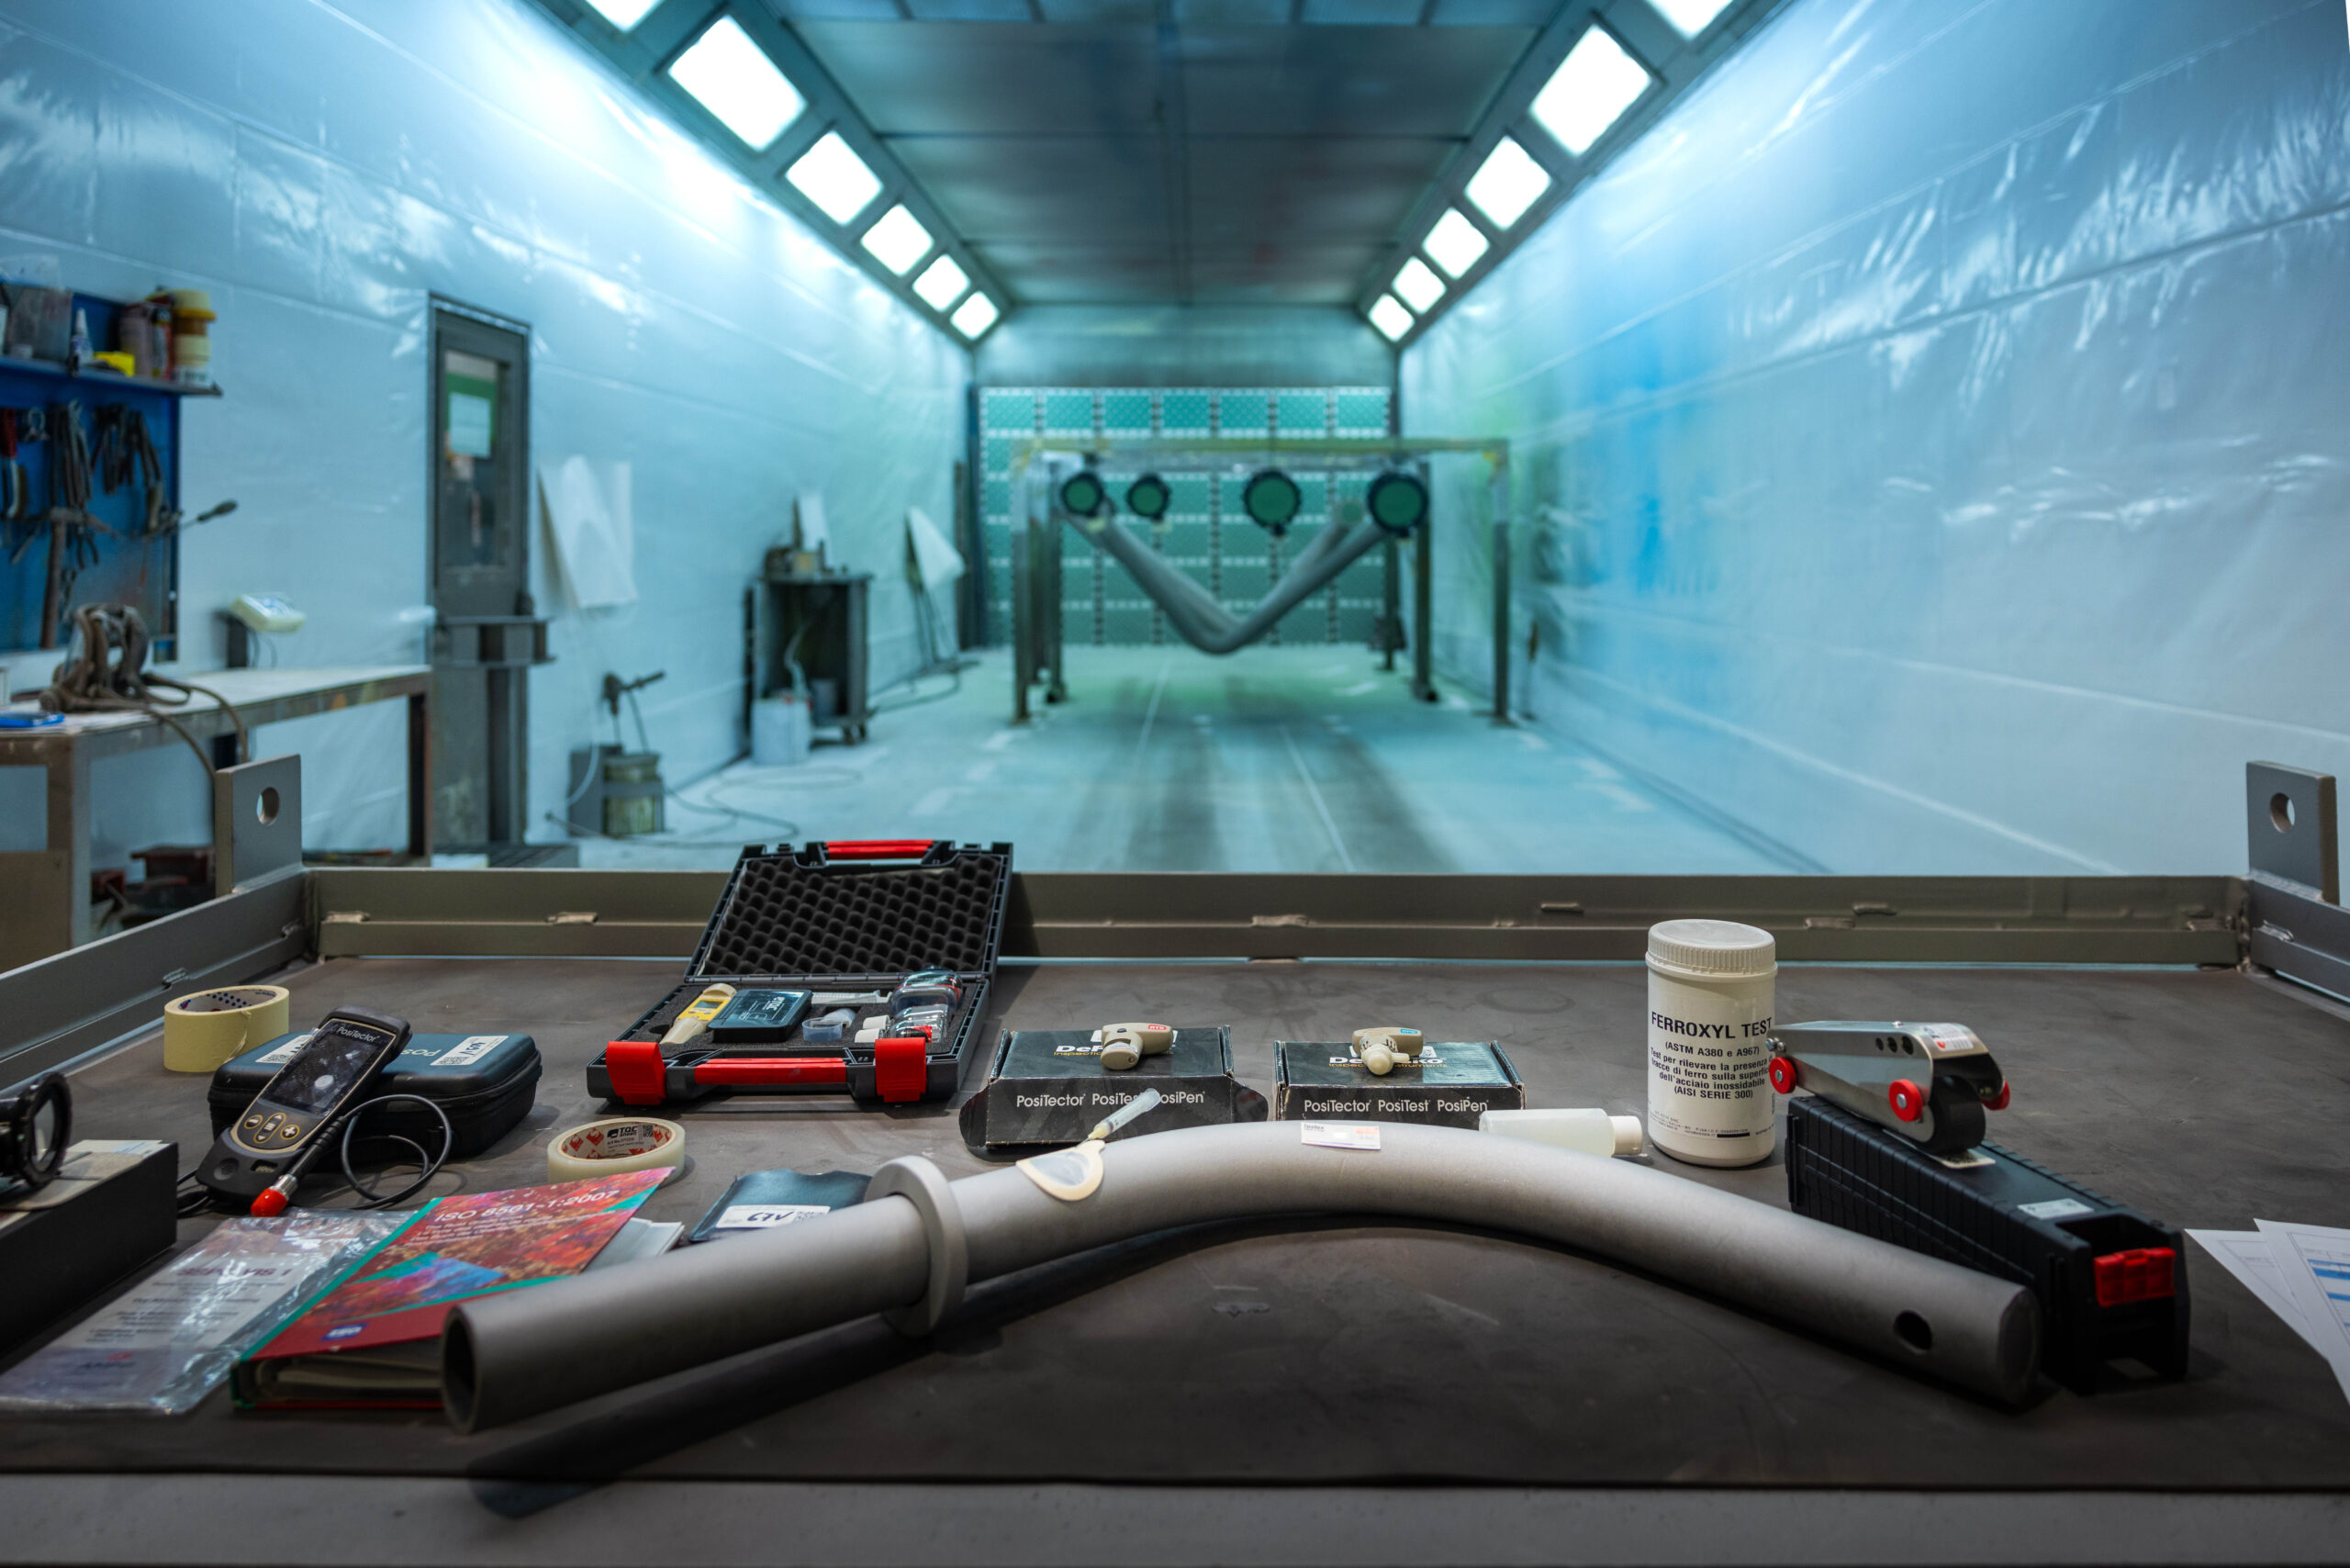
Following sandblasting, tests are performed and documented in accordance with relevant ISO standards to verify compliance with customer specifications, including:
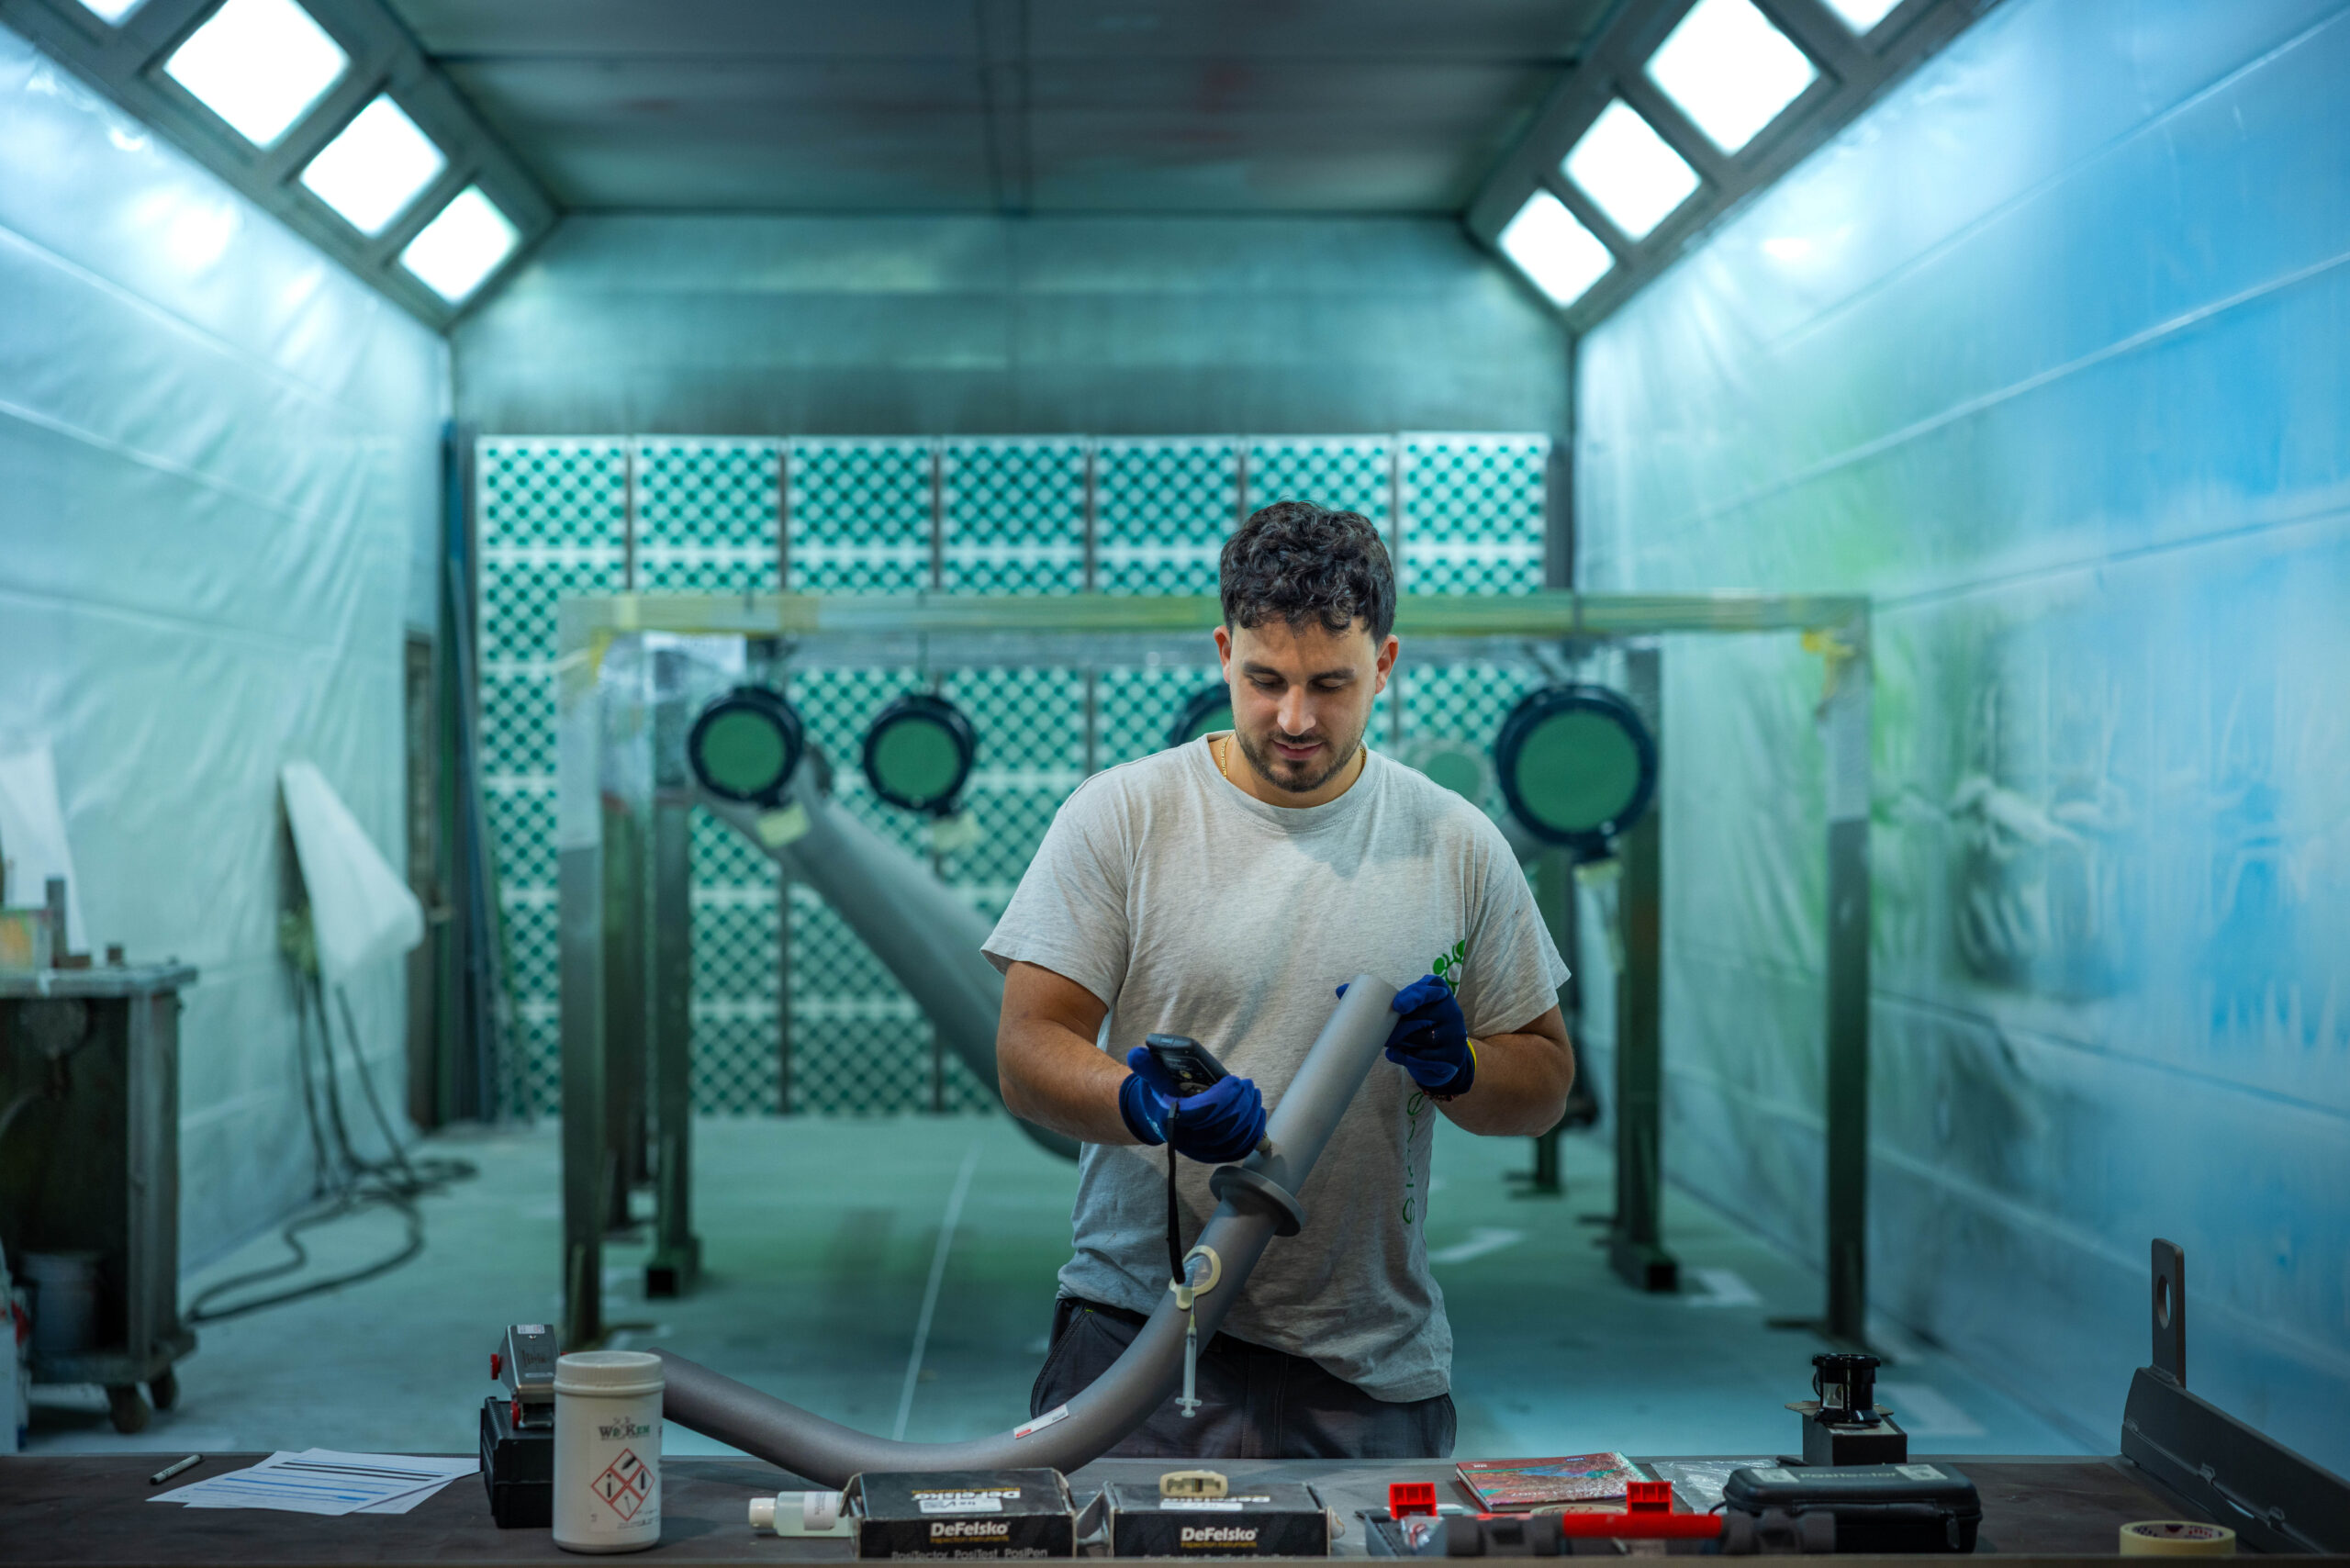
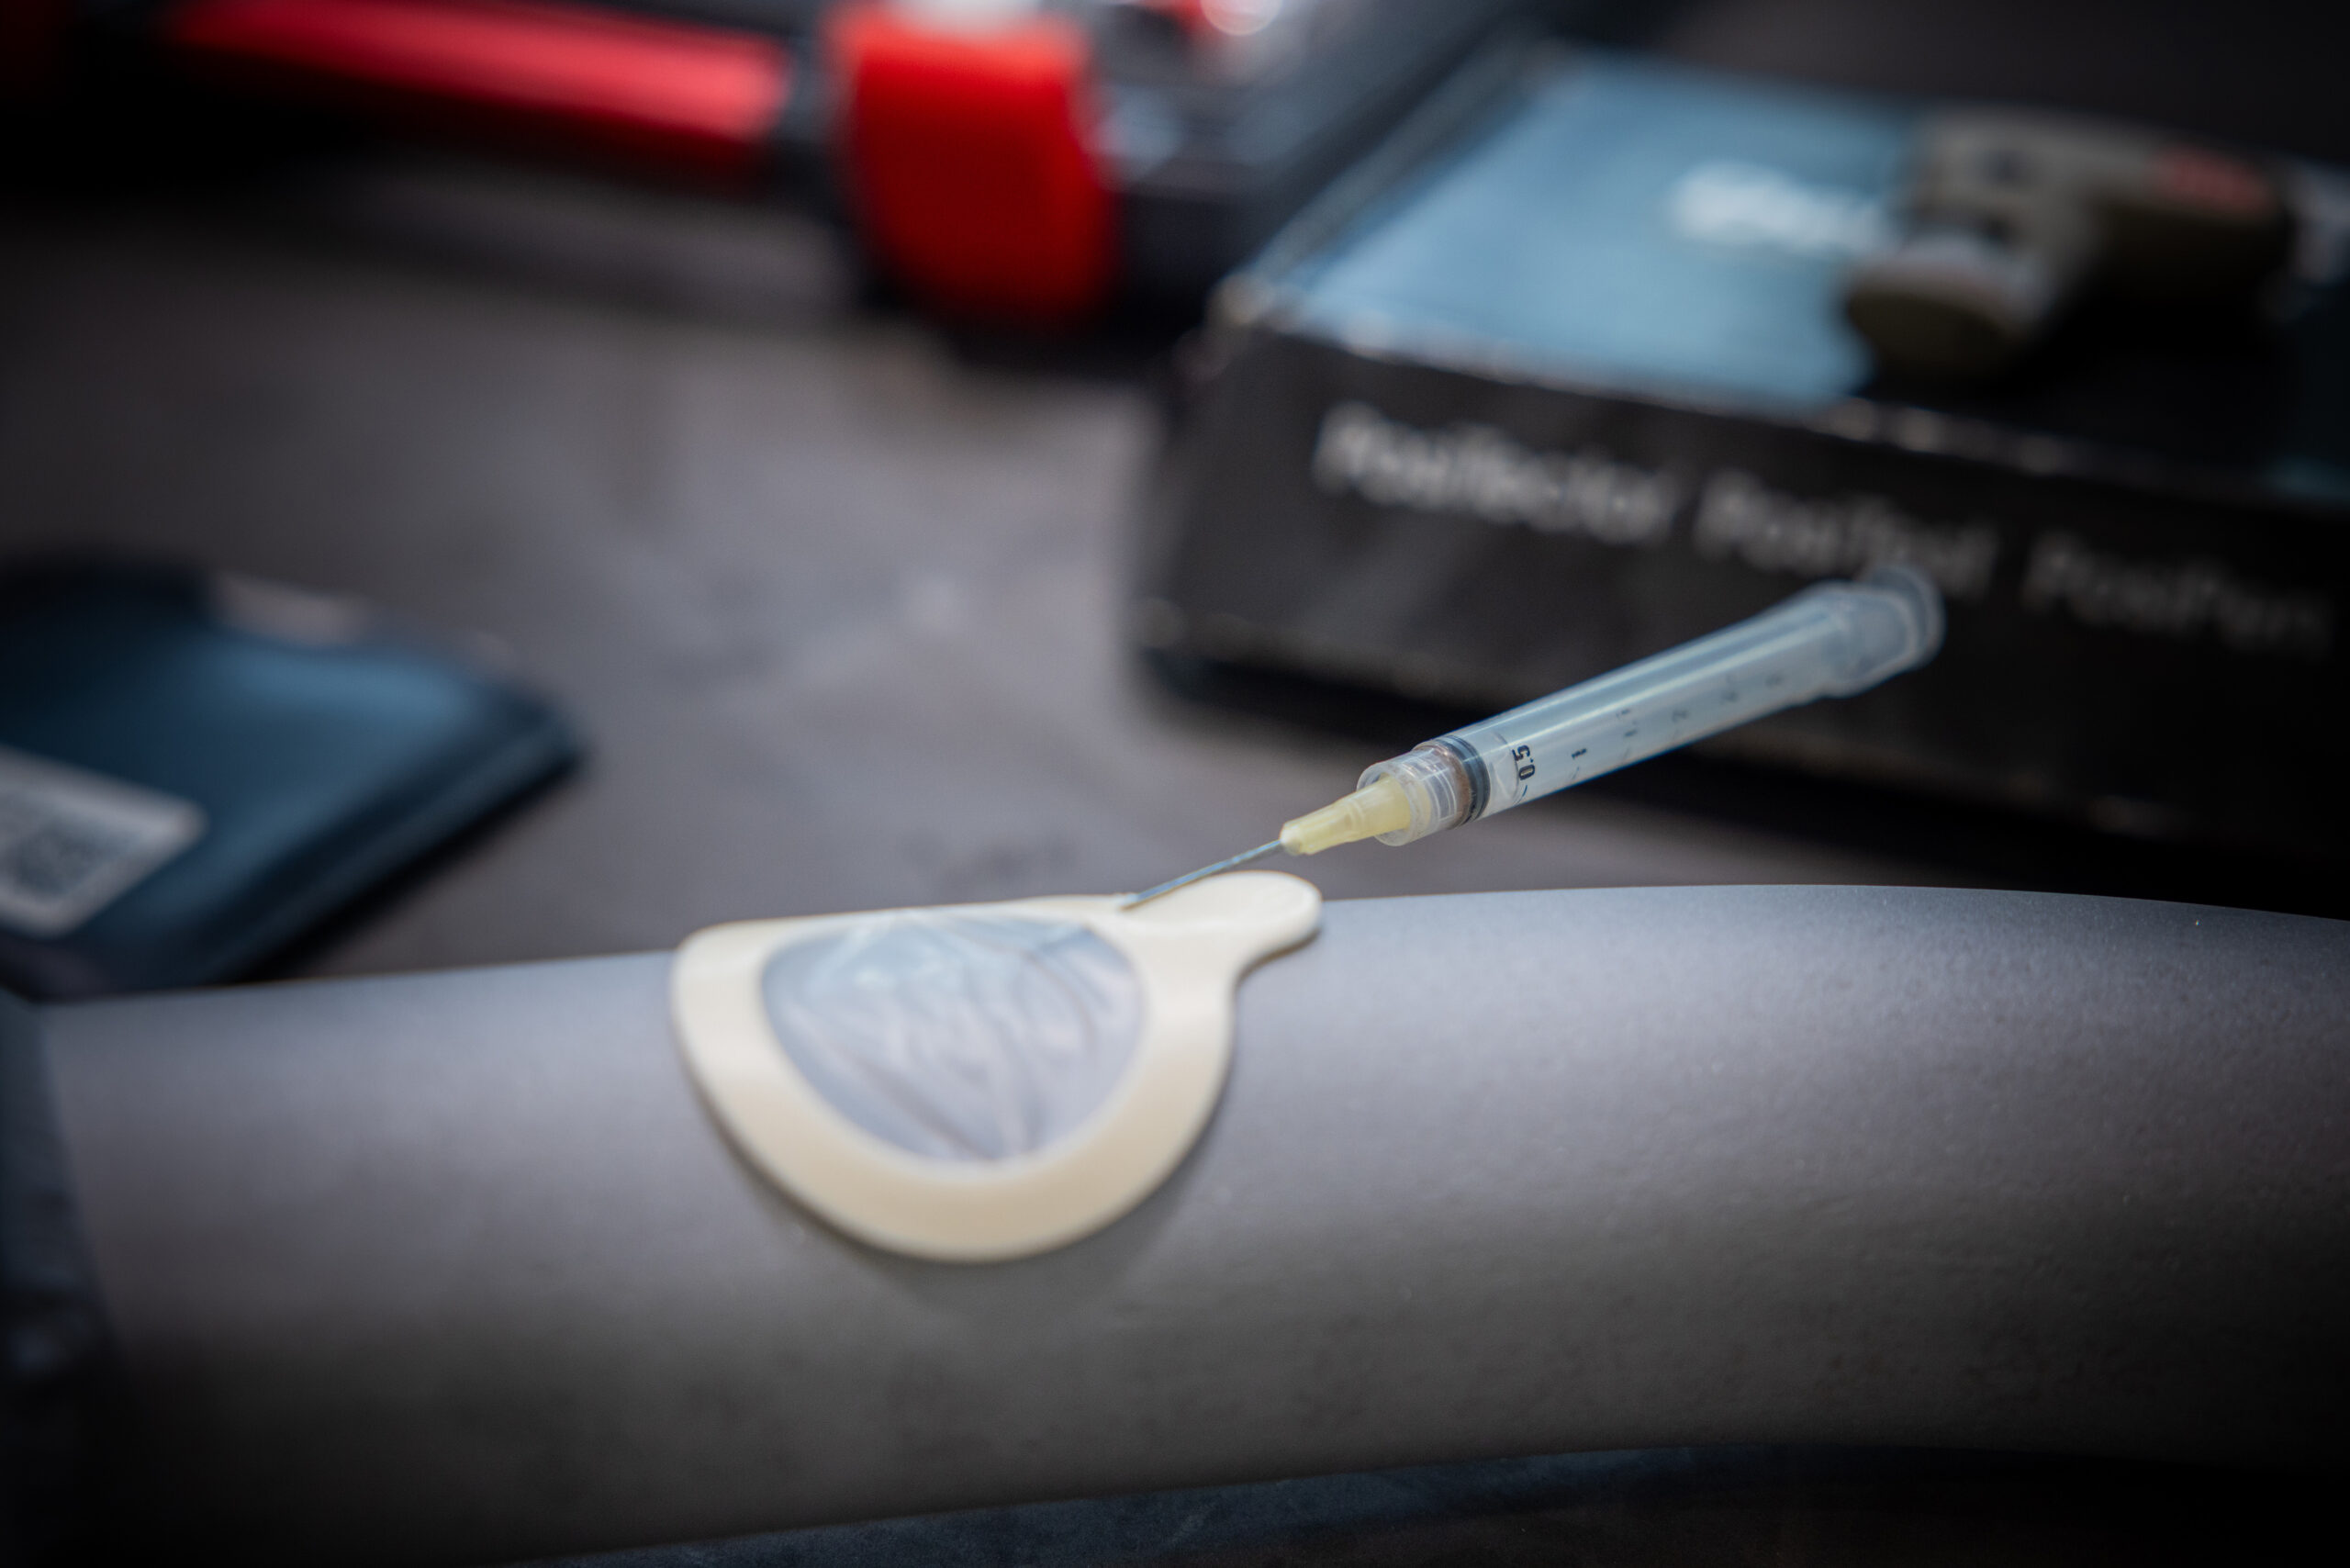
- WATER AND SALT TEST – An extraction cell is applied to the surface, and deionized water is injected using a syringe to dissolve and extract soluble salts. The solution is then recovered and analyzed by conductivity measurement to assess the level of soluble salt contamination.
- SURFACE DUST TEST – ISO 8502-3 – A specific adhesive tape is applied to the prepared surface under prescribed pressure and assessed in accordance with the applicable standard to determine dust quantity and particle size.
- SURFACE PROFILE ASSESSMENT – ISO 8503 SERIES – Following abrasive blasting, the surface profile is measured using the replica tape method in accordance with ISO 8503-5 to ensure compliance with the specified surface roughness requirements for optimal coating adhesion.
PAINTING
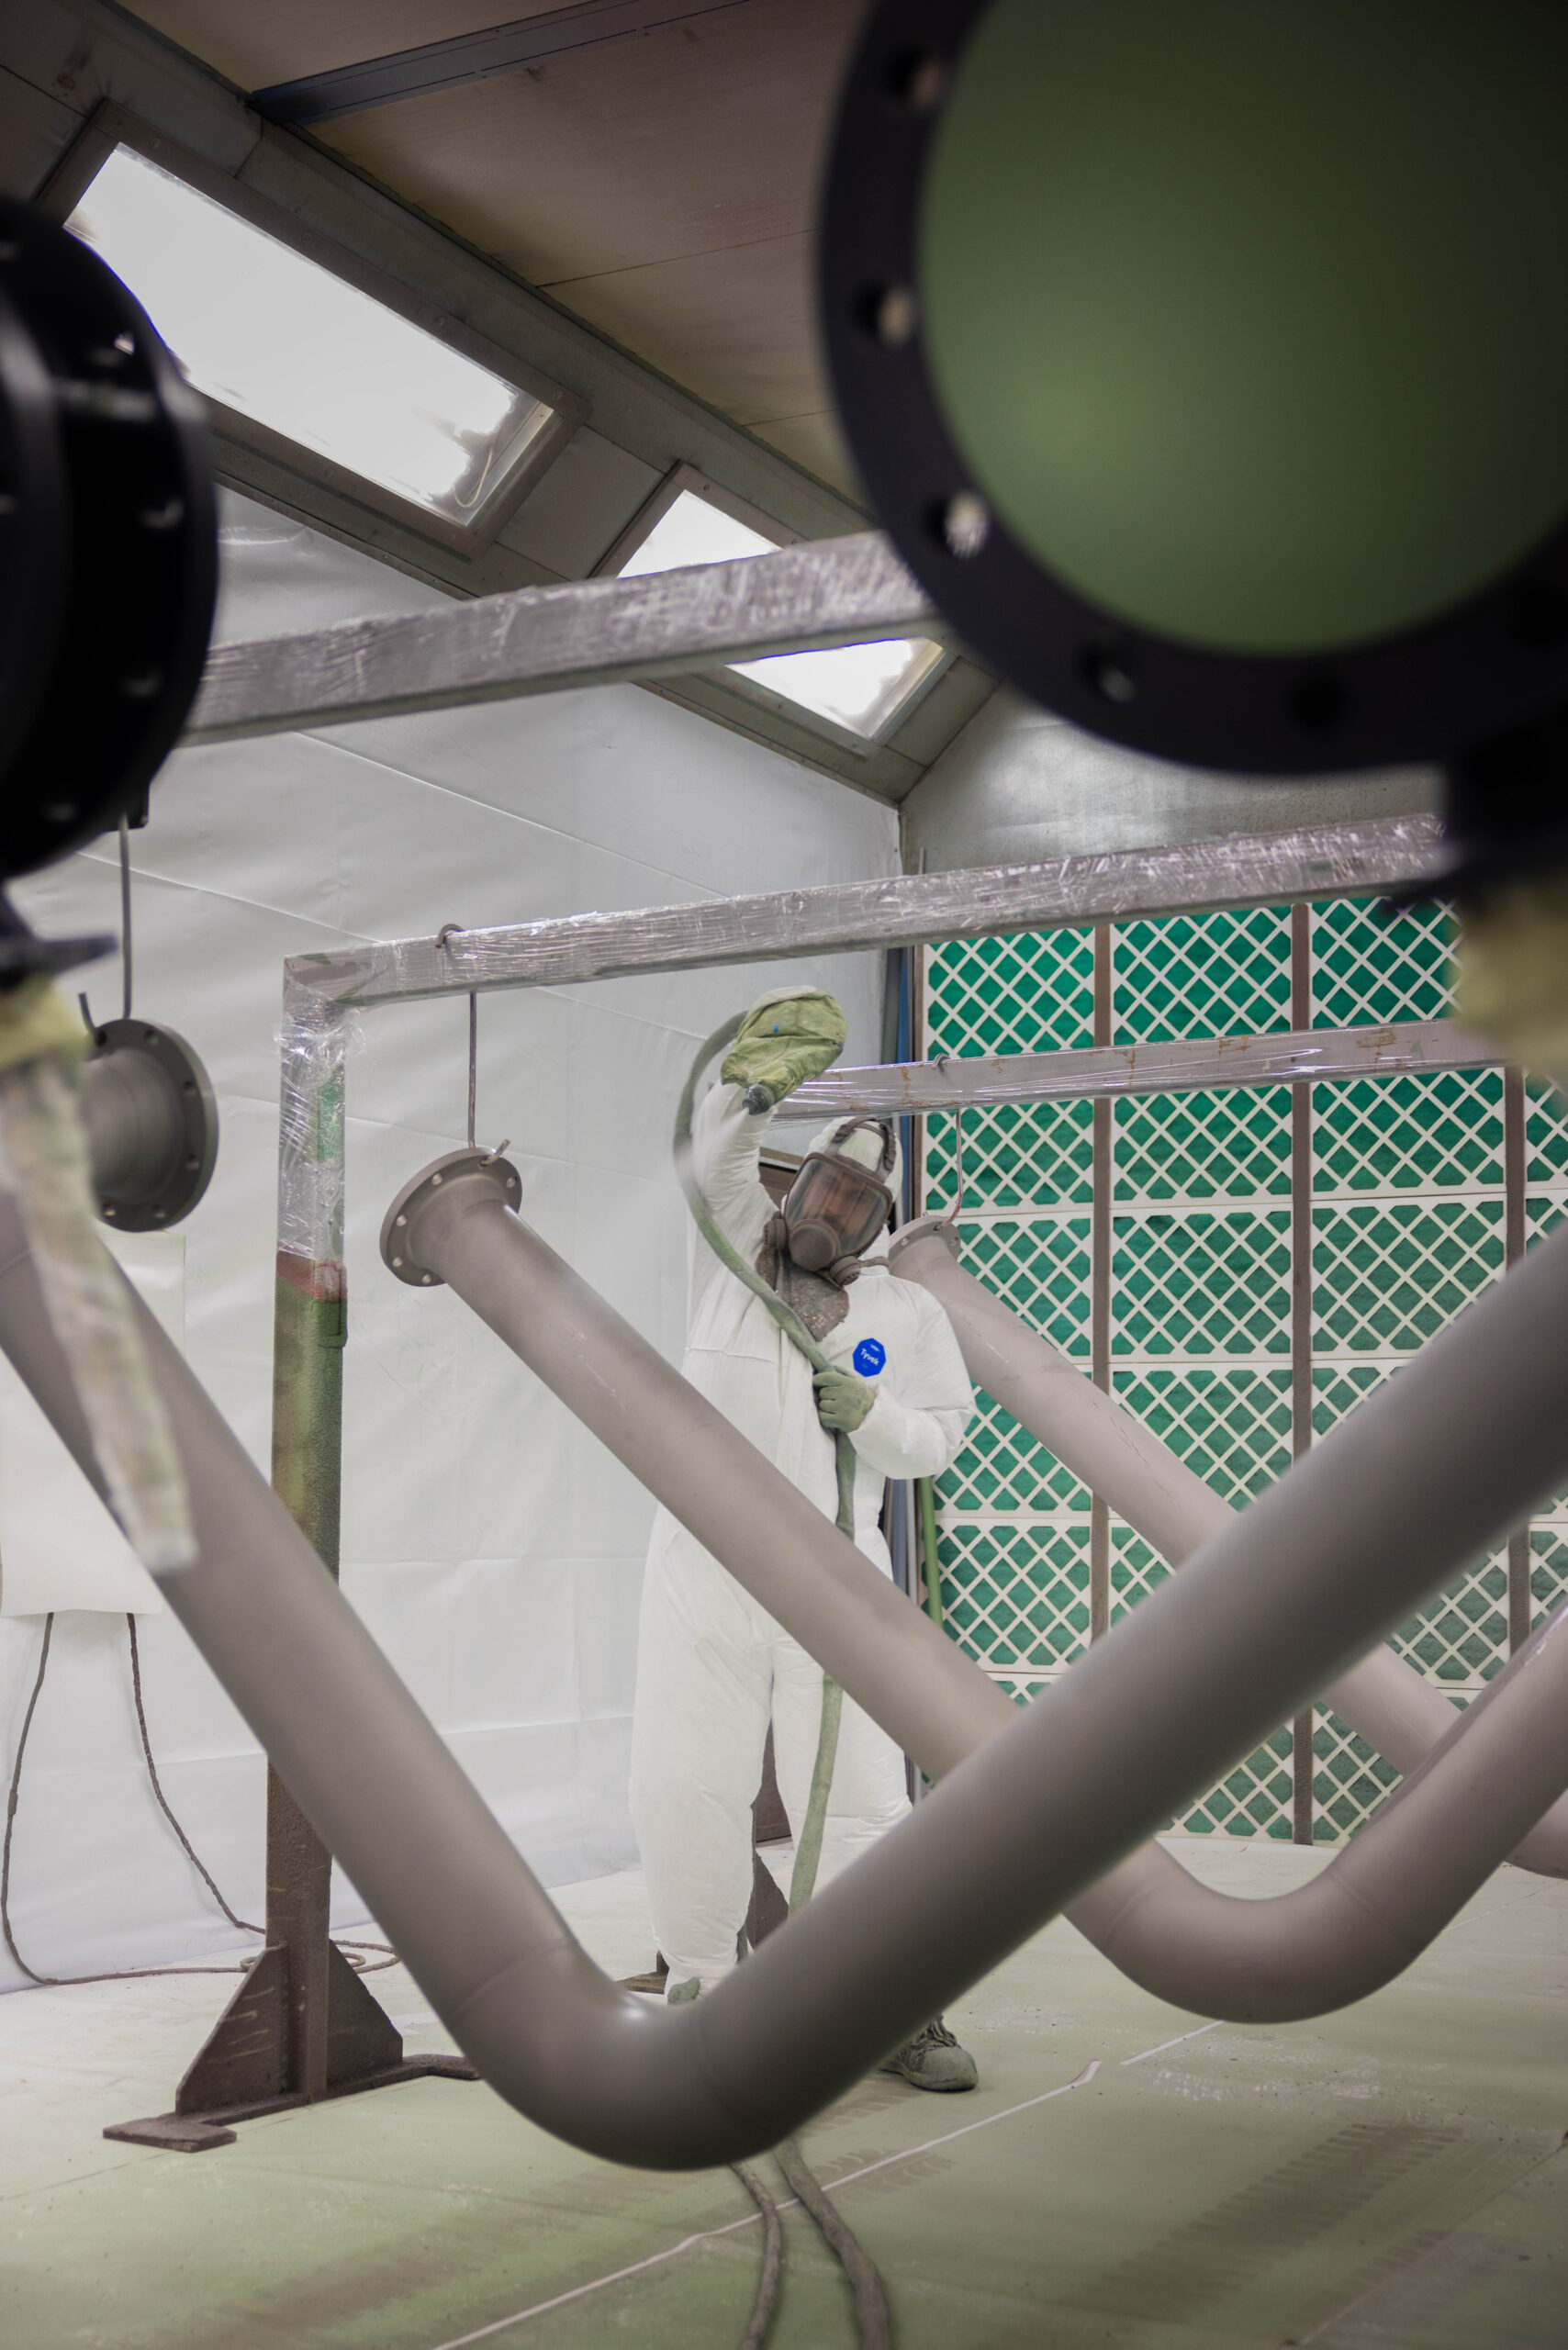
Painting is the second stage of the process, divided into a three-coat painting system, usually, but not necessarily:
- Zinc-rich coat
- Epoxy coat
- Polyurethane top coat
The brand of all products applied is selected within the client’s vendor approved list.
The two underlying coats beneath the colored topcoat provide long-term protection against corrosion and chemical attack, ensuring a service life of up to 25 years.
The visible finish is mostly provided by a polyurethane coating, selected for its elasticity and chemical and mechanical resistance, color and gloss retention properties. The coating is applied in the colors specified by the customer for each item.
FINAL TESTING
The wet film thickness is checked during the application before the solvent evaporates, but it is the dry film thickness that confirms the quality of the process, measured after the specified drying or curing period, and verified against project specifications.
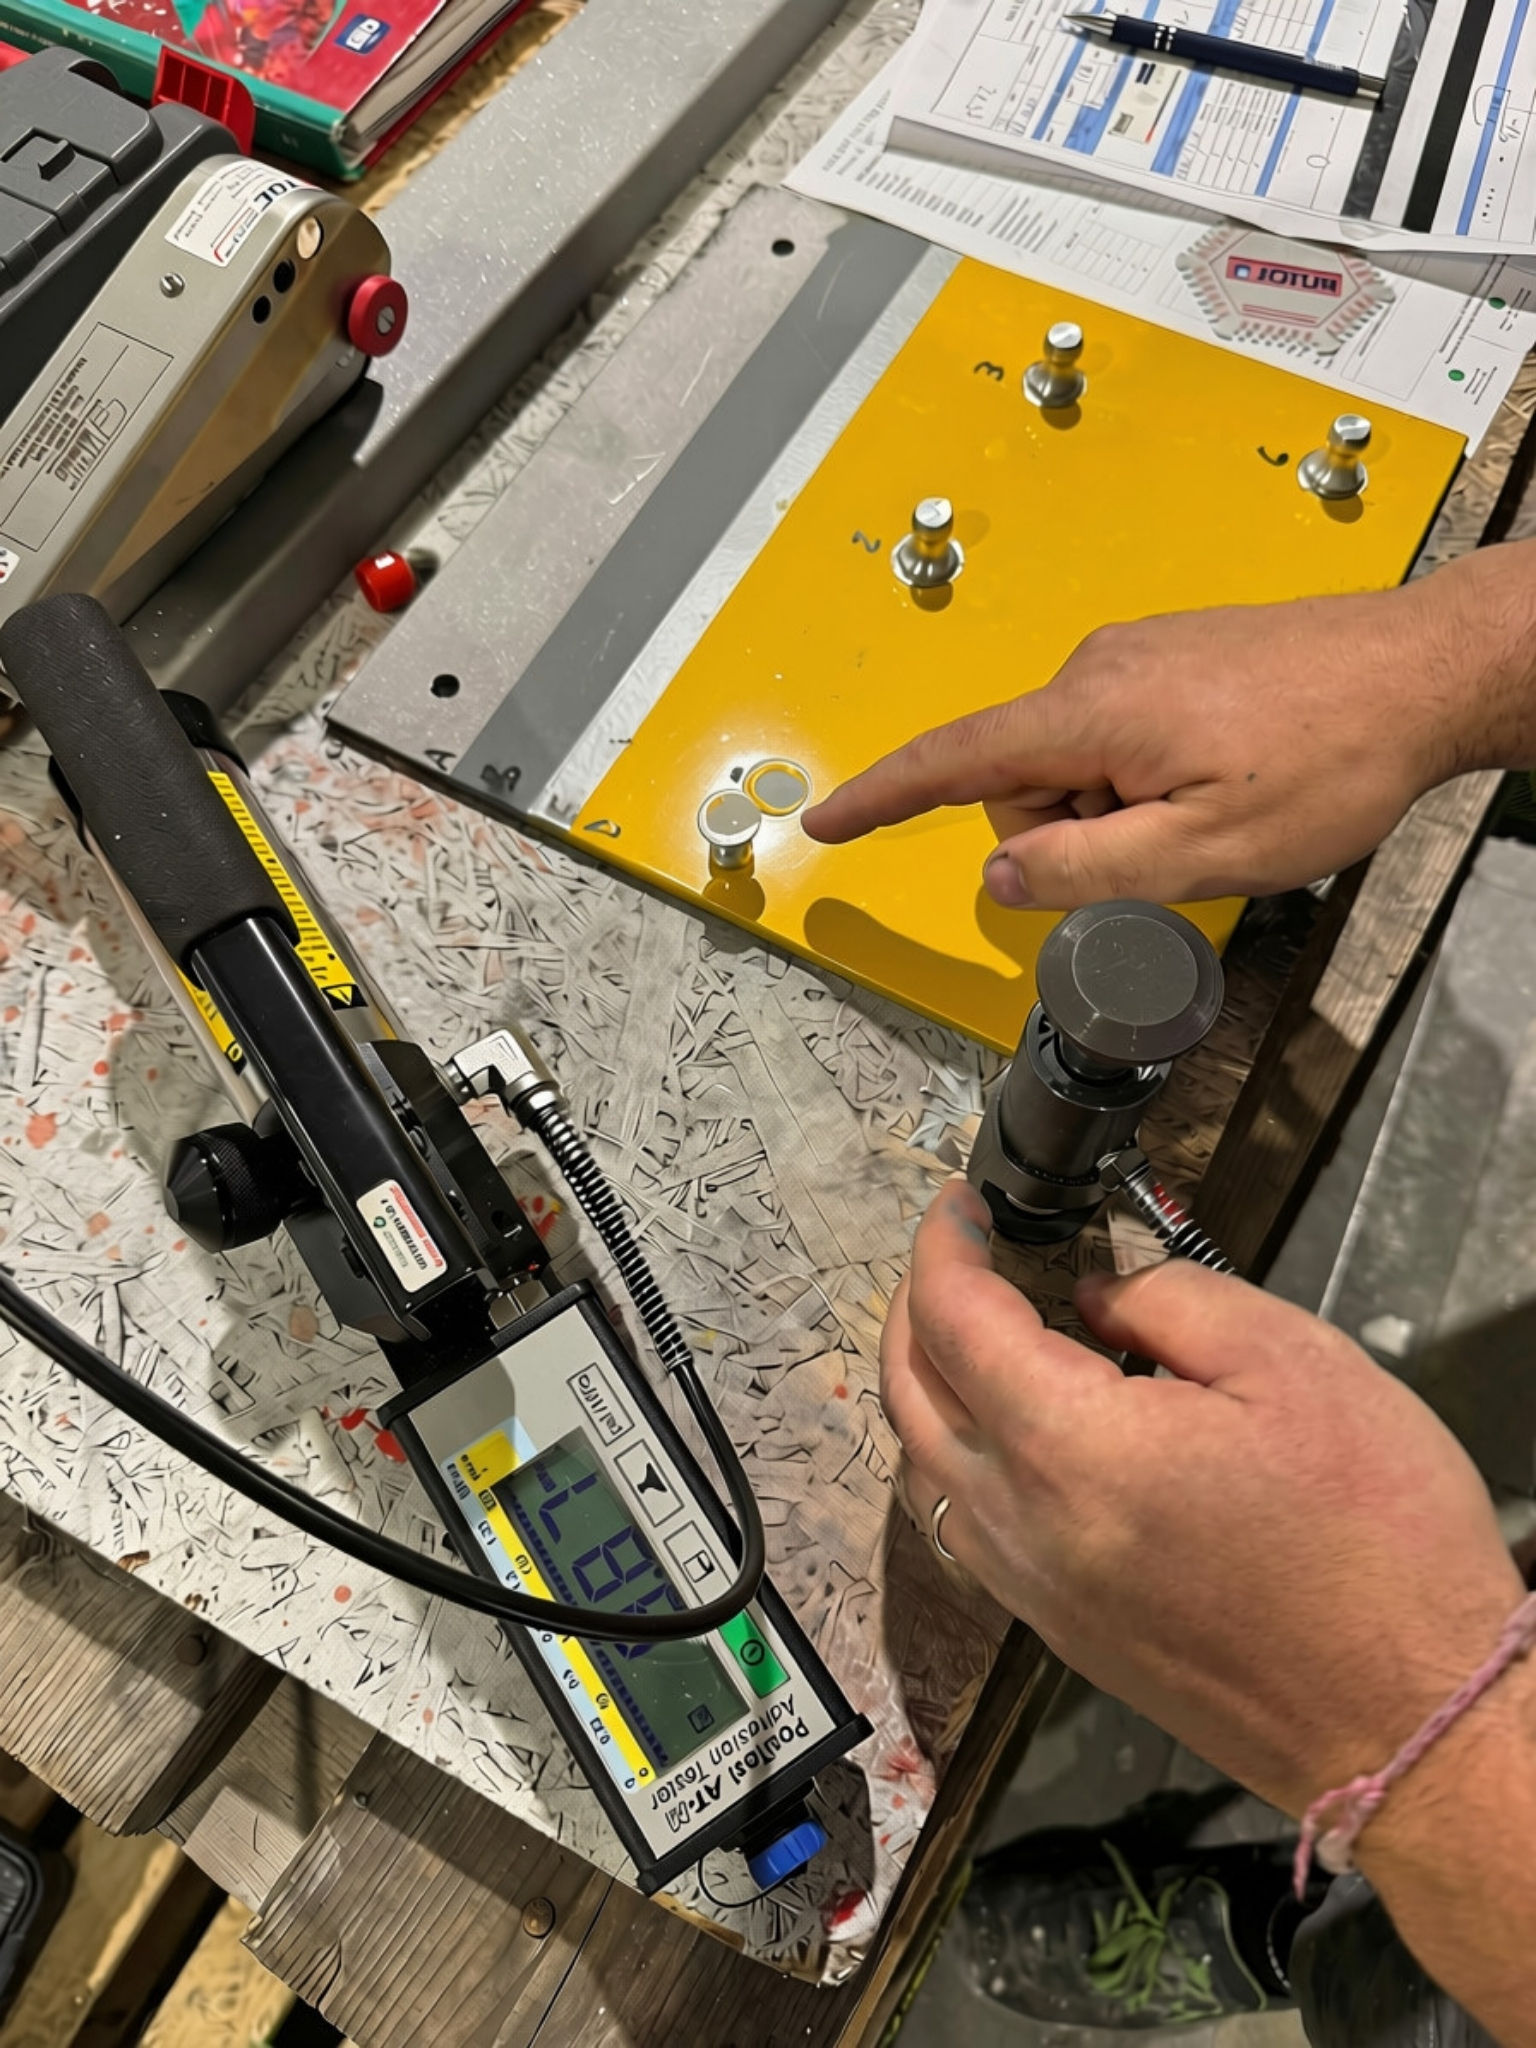
The final test is carried out some time after complete drying to assess the coating’s resistance to abrasion. This test involves the use of special suction cups operated by compressed air to determine the extent to which the coating has been removed from the treated metal when a pull-off occurs.
This is a highly meticulous procedure, which typically involves a single pull-off test on the polyurethane topcoat, while ensuring that the underlying epoxy and zinc-rich coating layers remain intact. The test is performed under controlled environmental conditions, with a temperature differential (ΔT) starting from 6°C.
A STRATEGIC CHOICE THAT BRINGS ADVANTAGES BEYOND QUALITY
Unlike most competitors that rely on subcontractors, Sinergia ensures direct control over all finishing processes. This enables us to meet the most stringent requirements of customers, turning this activity into a competitive advantage. Our capability to manage coating systems up to C5-VH ensures long-term protection in harsh marine environments and challenging industries such as oil and gas.
Directly managing all processes has driven continuous improvement as well, with a dramatic reduction in customer punch-list items. In case of rising painting issues during project execution, our experts can promptly set up corrective actions, minimizing delays that would occur in case of subcontracted supplies.
Would you like to learn more about our manufacturing process?
Contact us at marketing@sinergia-it.com


